Contact Us
Contact Us
Your Total Safe Patient Handling Partner
1000 Items
How to Choose a Chocopie Cake Production Line?
Choosing a Chocopie Cake Production Line is not just a matter of comparing machine speeds. It means matching mixing, baking, filling, coating, cooling, and packaging stages to the product you intend to sell. A small change in cake diameter can affect deposit accuracy, oven loading, and chocolate coverage. Details matter.
The scale of food waste makes process control worth examining. UNEP’s Food Waste Index Report 2024 estimates that 1.05 billion tonnes of food were wasted in 2022 across households, food service, and retail. That figure is not specific to cake factories, but it underlines why reducing rejects and avoidable losses deserves attention. A line that runs quickly but produces uneven shells may create more waste than it prevents. Faster is not always better.
A careful selection starts with measurable requirements: target output per hour, product dimensions, recipe characteristics, available floor space, and cleaning needs. Ask suppliers for trial data using a product close to your own, not only an ideal demonstration sample. Check how the line handles filling weight, coating thickness, cooling time, and packaging alignment. These details are easy to overlook. They are also costly to fix after installation. No single configuration fits every factory; the right choice depends on real operating conditions, and sometimes the first estimate needs revision.
Chocopie Cake Production Line Basics and Product Requirements
How to Choose a Chocopie Cake Production Line?
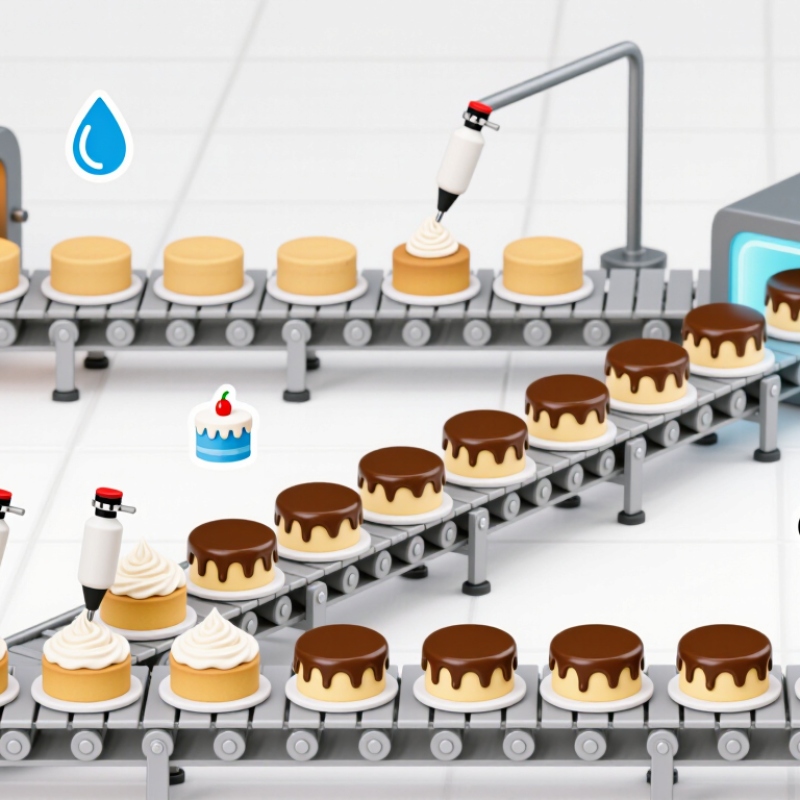
Choosing a Chocopie cake production line starts with the product, not the machine catalog. A typical cake has two soft layers, a cream filling, and a chocolate coating. Each part creates a separate process requirement. The line should control batter weight, baking temperature, cooling time, filling volume, coating thickness, and final setting. Ask for trial production using your own recipe. Small differences in batter moisture can change the cake’s bite.
Product requirements should be written as measurable targets. Define piece weight, diameter, height, filling ratio, coating tolerance, and acceptable breakage rate. Check whether the oven provides stable heat across the belt, not only near the door. Cooling must reduce the center temperature before filling and coating. Otherwise, cream may soften and chocolate may show dull patches. In my experience, operators often underestimate changeover time. A fast line may still lose hours during cleaning and adjustment.
Hygienic design is essential. Choose accessible surfaces, sealed bearings, food-grade contact materials, and drainage without standing water. Confirm that controls record temperature, speed, alarms, and batch data. Safety guards and emergency stops need practical testing, not paperwork alone. Leave room for inspection and maintenance. Many layouts disappoint here. Request samples from several operating conditions, including lower-speed runs and recipe variation. A reliable decision uses production evidence, service documentation, and realistic labor assumptions rather than maximum advertised capacity.
How to Choose a Chocopie Cake Production Line? - Chocopie Cake Production Line Basics and Product Requirements
| Production Stage | Main Equipment | Typical Product or Process Requirement | Typical Operating Range | Key Selection Criteria | Quality Check |
|---|---|---|---|---|---|
| Ingredient Preparation | Flour sifter, sugar pulverizer, weighing and batching system | Ingredients should be accurately weighed, sifted, and protected from foreign matter before mixing. | Batch accuracy: typically within ±1% for major ingredients; finer tolerance may be required for minor ingredients. | Choose equipment according to recipe size, dust-control needs, allergen segregation, and cleaning procedures. | Verify ingredient identity, weight, sieve condition, and batch records. |
| Batter Mixing | Planetary or high-shear batter mixer | The batter must be uniform, free of dry pockets, and suitable for depositing without excessive aeration. | Mixing time and speed depend on the formulation; batter temperature is commonly controlled near room temperature. | Consider bowl capacity, variable-speed control, scraper design, recipe repeatability, and ease of sanitation. | Check batter viscosity, density, color, and absence of unmixed ingredients. |
| Cake Sheet or Shell Forming | Depositor with multi-nozzle head and adjustable forming plates | Each cake piece should have consistent weight, diameter, height, and spacing on the baking band. | Typical deposited piece weight: approximately 10–30 g, depending on the finished product size. | Match nozzle count and depositing width with target output, product geometry, and batter viscosity. | Measure piece weight, dimensions, surface uniformity, and deposit position. |
| Baking | Continuous tunnel oven or rotary baking oven | The cake should be fully baked while retaining a soft, flexible crumb and a uniform golden-brown surface. | Typical baking temperature: approximately 160–210°C; residence time often ranges from 3–10 minutes. | Evaluate temperature-zone control, belt width, heating method, ventilation, energy use, and recipe changeover time. | Check internal doneness, moisture, color, thickness, and absence of burnt edges. |
| Cooling | Multi-level cooling conveyor or cooling tunnel | Cakes must be cooled before filling or coating to prevent filling softening and chocolate bloom. | Product temperature should normally be reduced to near the filling or coating room temperature before the next stage. | Size the conveyor for adequate dwell time and provide filtered, controlled airflow where practical. | Confirm core temperature, surface dryness, shape retention, and microbiological control requirements. |
| Filling | Cream or marshmallow depositor and sandwiching unit | Filling must be centered, stable, and evenly distributed between two cake shells. | Typical filling weight: approximately 20–50% of the assembled cake weight, depending on the recipe and product style. | Check filling temperature, viscosity range, pump compatibility, deposit accuracy, and quick-release cleaning design. | Measure filling weight, position, adhesion, leakage, and sandwich alignment. |
| Pre-Coating Conditioning | Short holding conveyor or conditioning tunnel | The assembled cake should be firm enough to pass through the coating system without deformation. | Product temperature and holding time depend on the filling type and coating formulation. | Provide adjustable conveyor speed, stable airflow, and hygienic access for product inspection. | Check firmness, surface condition, alignment, and absence of exposed filling that could contaminate the coating. |
| Chocolate Coating | Chocolate melting tank, tempering unit, enrober, and cooling tunnel | The coating should fully cover the cake, form a continuous shell, and maintain a clean appearance. | Dark chocolate is commonly tempered at approximately 31–32°C; milk and white chocolate generally require lower working temperatures. | Prioritize accurate temperature control, coating thickness adjustment, curtain stability, vibration control, and filtration. | Check coating coverage, thickness, gloss, snap, adhesion, and bloom after storage testing. |
| Final Cooling | Chilled-air cooling tunnel | The chocolate shell must set without condensation, cracking, or deformation. | Cooling conditions are commonly controlled with product-specific air temperature, humidity, and conveyor speed. | Select tunnel length and refrigeration capacity according to line speed, coating weight, room conditions, and product dimensions. | Inspect shell hardness, surface gloss, cracks, condensation, and product release from the belt. |
| Inspection and Rejection | Metal detector, checkweigher, vision inspection, and reject system | Finished products should meet weight, appearance, foreign-material, and packaging-line requirements. | Detection limits must be validated for the product, package format, equipment configuration, and applicable regulations. | Choose equipment with hygienic construction, data recording, automatic rejection confirmation, and easy verification. | Test certified test pieces, weight accuracy, reject timing, alarm function, and traceability records. |
| Primary Packaging | Horizontal flow wrapper or individual pouch packer | Packaging must protect the chocolate coating, preserve freshness, and provide a reliable seal. | Packaging speed should be matched to the upstream line, commonly with adjustable film registration and sealing temperature. | Consider product size variation, film type, seal width, gas flushing needs, coding system, and changeover time. | Check seal integrity, film alignment, date code readability, package appearance, and leakage resistance. |
| Secondary Packaging | Cartoner, case packer, or robotic packing cell | Individual packs should be counted, grouped, and placed into cartons without crushing or abrasion. | Case configuration should be selected according to sales format, pallet pattern, transport requirements, and warehouse handling. | Evaluate format flexibility, carton size range, robotic reach, accumulation space, and integration with conveyors. | Verify count accuracy, carton closure, label information, case weight, and pallet stability. |
| Hygienic Design | Food-grade conveyors, stainless-steel frames, washdown-compatible components | All product-contact areas should be accessible for inspection, cleaning, and sanitation. | Use materials and components suitable for the intended food-contact environment and cleaning chemicals. | Look for sloped surfaces, minimized crevices, tool-less access where possible, and separated electrical systems. | Review sanitation procedures, swab results, allergen controls, and preventive maintenance records. |
| Line Capacity Planning | Integrated production line with synchronized drives and controls | Rated capacity should reflect actual product weight, reject rate, changeover losses, cleaning time, and operating schedule. | Output is commonly stated in pieces per minute or pieces per hour; practical output is lower than nominal maximum speed. | Calculate required output using demand, operating hours, overall equipment effectiveness, and future expansion plans. | Compare accepted pieces per hour, downtime, waste percentage, changeover duration, and labor requirements. |