Why Choose a Certified Bandage Manufacturer?
Choosing a certified Bandage Manufacturer is a practical decision about patient safety, process control, and product consistency. A sterile bandage may look simple, yet its adhesive, absorbent pad, packaging, and seal must perform together. Small defects can cause contamination, skin irritation, or delayed wound care.
The World Health Organization’s Global Report on Infection Prevention and Control states that effective infection-control programs can reduce healthcare-associated infections by 35% to 70% in many high-income settings. This does not mean every bandage prevents infection. It does show why controlled manufacturing matters. ISO 13485 certification also requires documented quality systems, traceability, risk management, and corrective actions for medical-device production. These controls help buyers examine evidence, not attractive packaging.
Wound-care specialist Dr. Vincent Falanga has said, “Wounds are not just holes in the skin; they often signal an underlying disease.” That reminder changes how a buyer evaluates a supplier. A reliable Bandage Manufacturer should provide validated sterilization records, batch numbers, material specifications, and complaint-handling procedures. Ask for audits.
Certification is not a magic shield. It cannot replace clinical judgment, proper storage, or careful application. However, it creates measurable accountability. A manufacturer with transparent records can explain what happened to a roll of gauze from raw material to sealed carton. That level of detail supports safer purchasing decisions. The uncomfortable truth is simple: the cheapest product may become expensive when quality failures reach patients.
What Certification Means: ISO 13485:2016 and Medical-Device Quality Control
A certified bandage manufacturer treats quality as a controlled process, not a marketing claim. ISO 13485:2016 defines a medical-device quality system covering risk management, documented procedures, supplier controls, production, and post-market feedback. The ISO Survey 2022 recorded 38,972 valid ISO 13485 certificates worldwide. This figure shows broad adoption, but certification alone does not prove that every bandage is perfect.
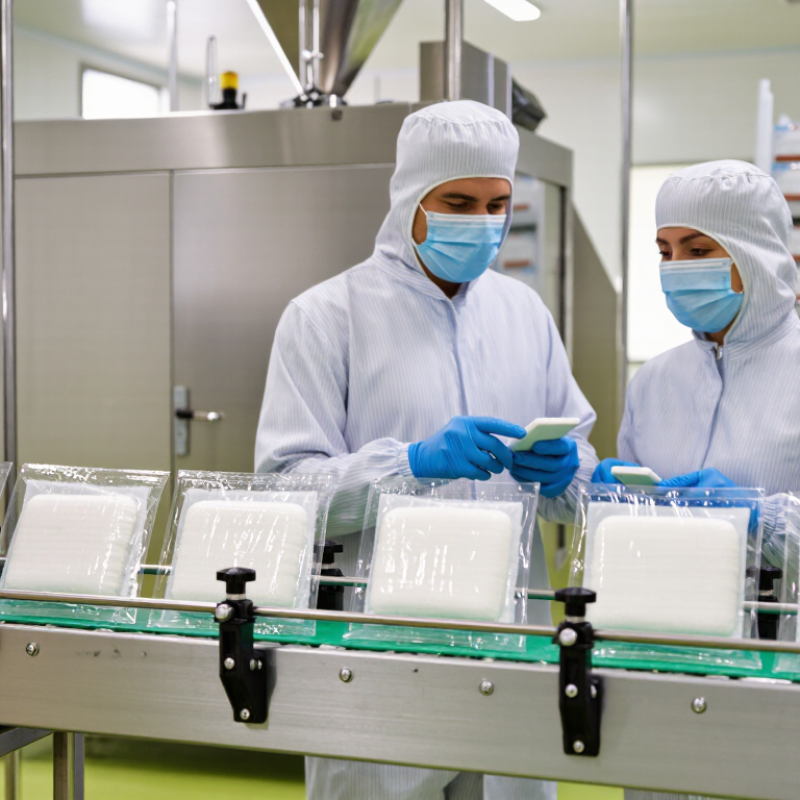
Look closely at the factory floor. Incoming gauze should have lot identification and inspection records. Adhesive materials need controlled storage, while finished packs require seal checks, visual inspection, and traceability. A strong manufacturer can connect one carton to its raw materials, operators, equipment, and release records. ISO 13485 also expects corrective and preventive action when failures appear. Small details matter.
They matter under pressure.
The World Health Organization’s Global Benchmarking Tool emphasizes documented, risk-based controls for medical products and regulators. For bandages, this means evaluating skin-contact materials, packaging integrity, contamination risks, and labeling accuracy. A certified supplier should provide audit evidence, not only a certificate copy. However, audits are snapshots. Human error, weak supplier oversight, or incomplete complaint analysis can still occur. That is why experienced manufacturers review trends, challenge their own procedures, and improve after near misses. Certification offers a reliable framework; disciplined daily execution gives it value.
Why Choose a Certified Bandage Manufacturer?
What Certification Means: ISO 13485:2016 and Medical-Device Quality Control
This chart shows the number of numbered subclauses in each major ISO 13485:2016 section. The standard covers quality management, management responsibility, resources, product realization, and measurement and improvement—helping manufacturers control processes throughout the medical-device life cycle.
Regulatory Compliance: FDA 21 CFR Part 820 and Risk-Based Production
Why Choose a Certified Bandage Manufacturer?
A certified bandage manufacturer builds quality into daily production, not just final inspection. Under FDA 21 CFR Part 820, documented procedures support design control, purchasing, production, and corrective action. These controls help connect each finished bandage to its materials, equipment, and operators. Lot traceability matters when adhesive performance or packaging integrity requires investigation.
Risk-based production makes these requirements practical. A manufacturer should identify hazards such as skin irritation, weak adhesion, contamination, and damaged sterile barriers. Each risk needs a proportionate control. Operators may check adhesive coating weight, seal strength, and package appearance during production. Quality teams can review environmental records and test samples before release. Small deviations should trigger documented evaluation, not informal approval.
Certification is useful evidence, but it is not the whole story. FDA does not simply certify every manufacturer as compliant. Reliable suppliers maintain an effective quality system and can explain how it works. Ask for objective records, change-control history, supplier evaluations, and CAPA effectiveness checks. Look closely.
Even mature systems can miss a supplier variation or overlook a repeated packaging defect. That is where honest review matters. A strong manufacturer investigates root causes, records uncertainty, and improves controls before the issue grows. Regular audits, trained personnel, and clear production records provide practical evidence of experience and professional discipline.
Patient Safety: ISO 10993 Biocompatibility Testing for Bandage Materials
Why Choose a Certified Bandage Manufacturer?
Patient safety begins with materials that touch damaged skin. The World Health Organization reports that one in ten patients experiences harm during healthcare, and about half of this harm is preventable (WHO, Global Patient Safety Action Plan 2021–2030). A bandage may look simple, but its adhesive, backing, ink, and absorbent pad can contact wounds for hours.
ISO 10993 biocompatibility testing helps evaluate these risks. The FDA’s Use of International Standard ISO 10993-1 guidance recommends a risk-based biological evaluation. Testing may include cytotoxicity, skin sensitization, and irritation, depending on contact type and duration. A certified manufacturer should connect each result to the actual finished bandage, not only to a raw material sample. Traceable batches, controlled production, and documented change management matter. A certificate is not magic. Testing can still miss a problem when suppliers change quietly.
Tips: Ask for recent ISO 10993 reports, material declarations, and batch traceability records. Check whether testing covers the complete product. Review adhesive and ink changes carefully. Independent laboratory evidence adds confidence, but it does not replace practical quality checks. Experienced manufacturers should also explain test limitations in plain language. That honesty is useful. Sometimes, the uncomfortable answer is the safer one.
Why Choose a Certified Bandage Manufacturer? - Patient Safety: ISO 10993 Biocompatibility Testing for Bandage Materials
| ISO 10993 Evaluation Area | Relevant Standard | What Is Evaluated for a Bandage | Typical Evidence or Method | Patient-Safety Relevance |
|---|---|---|---|---|
| Biological evaluation planning | ISO 10993-1 | The bandage’s contact type, contact duration, materials, intended use, and exposure route. | Documented biological evaluation plan based on the finished device, including skin-contact conditions and risk assessment. | Ensures that testing is selected according to the actual patient-contact scenario rather than applied as a generic checklist. |
| Chemical characterization | ISO 10993-18 | Substances that may migrate from adhesives, backing films, nonwoven layers, colorants, coatings, or packaging-contact materials. | Material and extractables assessment using appropriate analytical techniques, such as chromatographic or spectrometric methods. | Helps identify potentially hazardous constituents before deciding whether additional toxicological or biological testing is needed. |
| Toxicological risk assessment | ISO 10993-17 | Potential health risks associated with identified chemical constituents and estimated patient exposure. | Toxicological evaluation considering dose, exposure duration, route of exposure, and available hazard information. | Supports science-based decisions about whether detected substances present an unacceptable risk. |
| Cytotoxicity | ISO 10993-5 | Whether substances released from the bandage adversely affect cultured mammalian cells. | In-vitro cell-response testing using an extract or direct-contact approach, with appropriate controls. | Can reveal harmful leachables or residues that may damage cells at the skin or wound interface. |
| Skin sensitization | ISO 10993-23 | Potential for contact allergens from adhesives, rubber-based components, preservatives, dyes, or other materials to trigger sensitization. | Assessment of sensitization potential using a justified combination of chemical characterization, toxicological review, and relevant biological methods. | Reduces the risk of delayed allergic skin reactions after repeated or prolonged use. |
| Skin irritation | ISO 10993-23 | Potential for temporary or persistent local irritation caused by the finished bandage or its extractables. | Irritation evaluation selected according to the device’s intended contact and exposure conditions. | Helps distinguish acceptable skin contact from reactions such as erythema, edema, or other local inflammatory responses. |
| Acute systemic toxicity | ISO 10993-11 | Whether substances released from the bandage could cause harmful effects beyond the application site. | Consideration of exposure assessment and, where scientifically justified, systemic toxicity testing using prepared extracts. | Provides evidence about risks that may not be visible as a local skin reaction. |
| Hemocompatibility | ISO 10993-4 | Interaction with blood when the bandage is intended to contact bleeding tissue or blood for a clinically relevant duration. | Assessment selected from relevant categories such as thrombosis, coagulation, platelets, or complement activation. | Important for dressings used on open or actively bleeding wounds where blood-material interactions may occur. |
| Particulate and residue control | ISO 10993-9 and applicable biological-evaluation principles | Potential release of fibers, particles, processing residues, or other foreign material from the finished product. | Risk-based characterization of particulate matter and manufacturing residues, supported by process controls and inspection records. | Helps reduce avoidable contamination and foreign-material exposure at the skin or wound site. |
| Change-control verification | ISO 10993-1 risk-management approach | Whether changes to adhesive formulation, substrate, coating, sterilization, packaging, or suppliers could alter biological safety. | Documented impact assessment, updated material information, and repeat testing or justification when required. | Helps maintain consistent safety performance across production batches and product revisions. |
Note: The specific ISO 10993 tests required for a bandage depend on its final materials, intended contact with intact or breached skin, contact duration, sterilization method, and documented biological risk assessment. ISO 10993 testing is not a substitute for manufacturing quality controls, process validation, or applicable regulatory requirements.
Product Performance: EN 13726 Tests for Absorption, Moisture, and Wear
Why Choose a Certified Bandage Manufacturer?
A certified manufacturer should prove product performance with documented EN 13726 testing. This standard evaluates absorbency, moisture vapour transmission, and waterproofness for primary wound dressings. These tests reflect real clinical pressures. Fluid must move away from the wound. The outer surface should remain reasonably dry. The dressing must also resist wear during movement.
EN 13726 results require careful reading. The standard provides test methods, but it does not create one universal pass mark for every bandage. A reliable technical file should identify the test fluid, sample size, test duration, conditioning method, and variation between samples. According to the NHS National Wound Care Strategy Programme, wound care in England cost about £8.3 billion during 2017–2018. Poor moisture control can increase dressing changes and waste. That figure gives testing practical importance, not merely paperwork.
Tips: Ask for complete EN 13726 reports, not only a certificate number. Check absorption capacity alongside moisture vapour results. Review wear testing after flexing or handling. A clean laboratory result can still miss real-world problems. I would question results without variability data. Small details matter. Choose a manufacturer that combines certified processes, traceable batches, and experienced quality review. The European Committee for Standardization’s EN 13726:2023 framework supports this evidence-based approach, although clinical suitability still depends on wound type, exudate level, and professional assessment.
Traceability and Reliability: UDI Records, Batch Control, and Audits
Why Choose a Certified Bandage Manufacturer?
Traceability begins before a bandage reaches a clinic. A certified manufacturer assigns each product a Unique Device Identifier, or UDI, where applicable. The UDI links the item to its material history, production date, packaging line, and expiration date.
The FDA describes UDI as a system designed to identify medical devices through distribution and use. That matters when a single carton contains hundreds of dressings. One scan should reveal the batch, not create another question.
Batch control adds a practical safety barrier. Operators can record adhesive checks, sterile barrier inspections, and final packaging results against one lot number. If a deviation appears, staff can isolate affected cartons quickly. Small details matter. A missing seal is not small.
The World Health Organization’s Global Patient Safety Report 2024 estimates that one in ten patients experiences harm in healthcare, with more than half considered preventable. Reliable records cannot remove every risk, but they can shorten the distance between a defect and corrective action.
Audits test whether procedures exist beyond paperwork. ISO 13485-based quality systems require documented processes, training records, nonconformance handling, and corrective actions. Independent auditors may inspect production rooms, calibration logs, sampling plans, and complaint files.
A certificate alone is not magic. An honest manufacturer should explain audit scope, certificate validity, and batch-release controls. It should also admit weak points. Records can be incomplete, labels can be misread, and human review still matters. That uncomfortable reality is why traceability needs repeated verification, not one impressive audit.